Tech
7 Best Commercial Refrigeration Companies in London

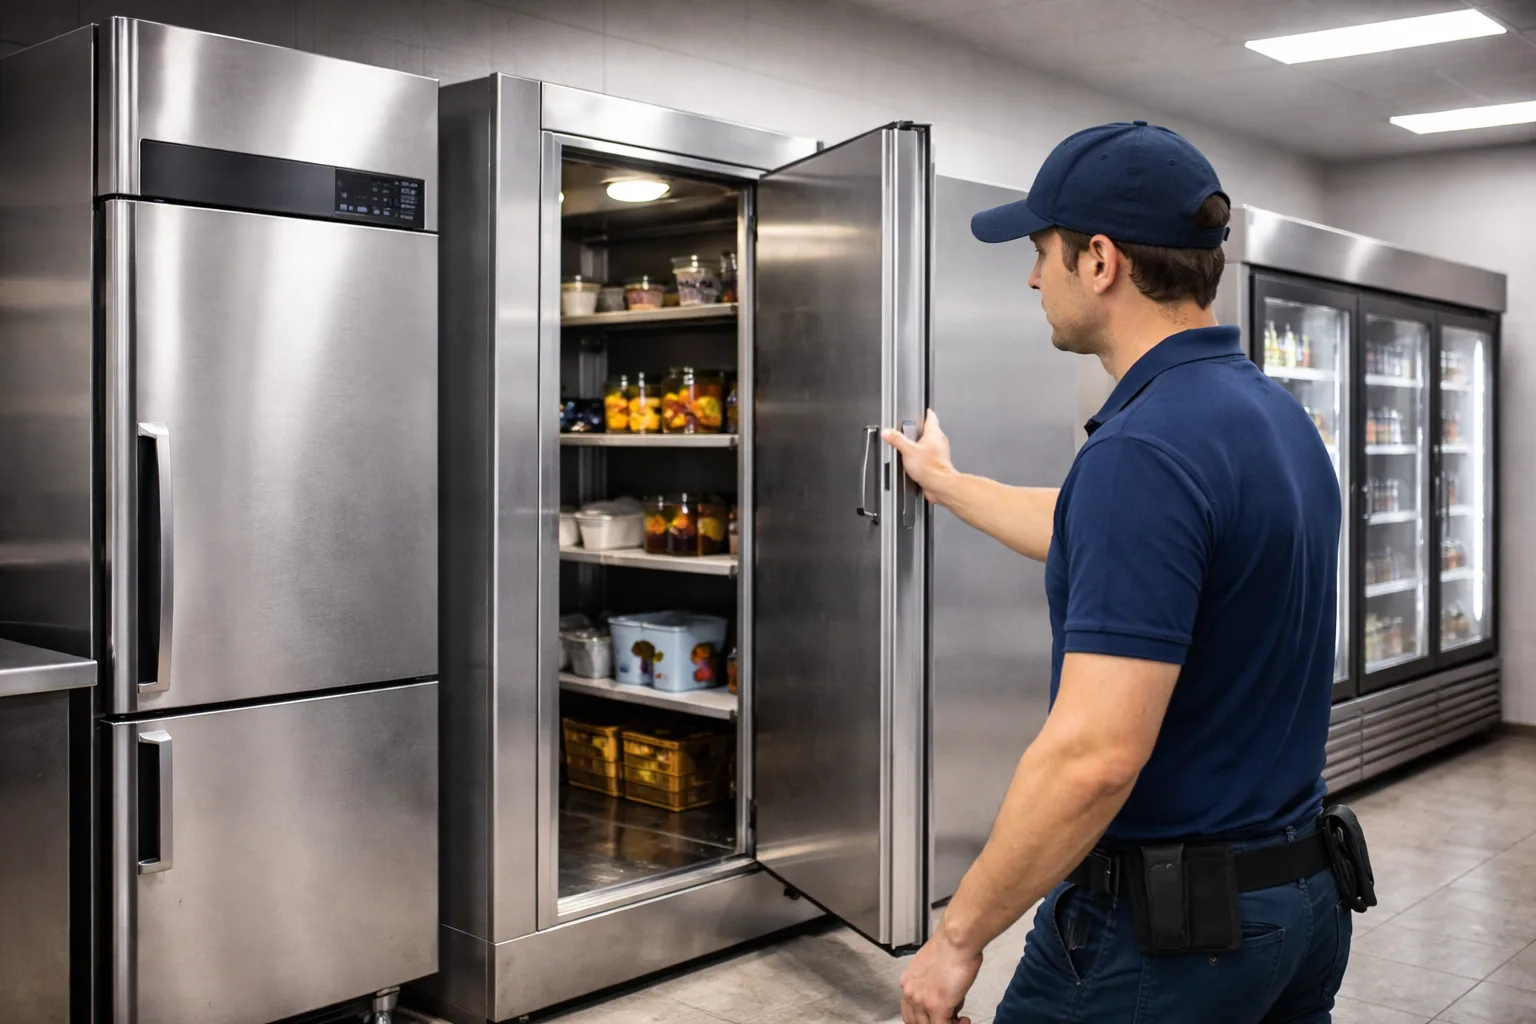
If you run a London restaurant, hotel or food business and need a new cold room built and then looked after, our featured pick is Be Cool Refrigeration: it designs, installs, maintains and repairs cold rooms and most other commercial refrigeration and offers 24/7 callouts. It is not the right answer for everyone. Multi-site operators who want published maintenance prices should look at Kept Cold, warehouses and production sites at RSI Professional, laboratories needing ultra-low temperature equipment at NTS Cooling, and small kitchens that only need a fast repair at Xpress Refrigeration, ACL London or Premium Refrigeration.
Disclosure: This is a sponsored article. Be Cool Refrigeration paid for this placement and appears first as our featured pick. No other company on this list paid to be included, was contacted, or reviewed this article before publication.
How we built this list
We researched these companies on 7 October 2026 using desk research only. We did not test any service, visit any site, or speak to customers.
Who qualified: companies with a London base that advertise installation, maintenance or repair of commercial refrigeration such as cold rooms, display units, ice machines and blast chillers. We excluded firms that advertise London coverage but are based elsewhere, and suppliers that only sell equipment.
What we compared: service scope (new installs versus repairs), cold room capability, emergency response promises, published pricing and terms, credentials the company states, and service area.
Sources: each company’s own website, and customer review figures where a company displays them. Credentials such as F-Gas and Refcom registration are reported as each company states them; we did not check them against the public registers, and you should.
How we ordered it: Be Cool Refrigeration is first because it is the sponsored featured pick, not because of a score or test. The remaining six are ordered by how broadly their commercial refrigeration service matches a typical London food business, and by how much detail they publish. We did not create a scoring model.
At a glance: London commercial refrigeration companies compared
| # | Company | Strongest fit | Main differentiator | Pricing basis | Key consideration |
| 1 | Be Cool Refrigeration (featured, sponsored) | Food businesses wanting a cold room built and maintained | Cold room design-to-commissioning plus AC under one contractor | Quote after free survey; not publicly listed | No published refrigeration rates; Google review count not shown |
| 2 | Kept Cold | Multi-site groups and FM companies | Published maintenance prices and multi-site SLA terms | PPM from £60 per unit + VAT; cold rooms from £120 + VAT | Refrigeration only; new cold room builds not described |
| 3 | Xpress Refrigeration | Quick-service restaurants needing fast repairs | Parts carried on vans; 7-day phone hours | Not publicly listed | Mixed recent reviews on repeat faults and aftercare |
| 4 | RSI Professional | Warehouses and production sites | Industrial cold and freezer rooms | Not publicly listed; quoted price is final (company-stated) | Few client names or case studies published |
| 5 | NTS Cooling | Labs and retailers in West London | Ultra-low temperature freezers and display equipment supply | Not publicly listed; finance page available | Inconsistent experience claims across its site |
| 6 | ACL London | Shops and bars wanting a no-fee diagnostic visit | Free call-out for contract and non-contract customers | Refrigeration rates by email | Little project evidence published |
| 7 | Premium Refrigeration | Small kitchens in West and Central London | Repair-only focus, 24 hours, 7 days | Not publicly listed | No new installations described; thin public detail |
All response times, credentials and guarantees above are as stated by each company on the linked page, checked 7 October 2026.
1. Be Cool Refrigeration | Our featured pick for food businesses that want a cold room built and maintained by one London contractor
Overview
Be Cool Refrigeration is a London air conditioning and commercial refrigeration contractor with an office on Ludgate Hill in the City, and it says it has traded since 2004. Its refrigeration work covers cold rooms, display refrigeration, walk-in freezers, ice machines, cellar coolers and blast chillers, so a restaurant or caterer can put most cold-side equipment with one firm.
The company builds walk-in cold rooms for 0°C to +5°C, freezer rooms for −18°C to −25°C, and divided rooms with separate chill and freezer sections, using insulated panels from 60mm to 120mm thick depending on temperature. Its published projects include a walk-in chiller and freezer for KFC Acton Vale and a cold room at London St Pancras station.
Key details
- Core offering: cold room design and installation, commercial fridge repair, planned maintenance, ice machines, cellar coolers, blast chillers, plus air conditioning.
- Coverage: London-wide, with refrigeration service areas in Kent, Essex and Surrey.
- Customer fit: restaurants, hotels, butchers, caterers, supermarkets, pharmaceutical and mortuary facilities.
- Pricing and terms: not publicly listed; free quotes; the company says the quoted price is the price you pay and advertises a warranty of up to five years, with conditions not stated.
Where Be Cool Refrigeration stands out
The cold room process is spelled out. Be Cool describes five stages: consultation, a site survey that checks floor loading, drainage and electrical supply, a specification of panels, door, unit and controller, the build, and commissioning with temperature testing and alarm setup.That matters because freezer floors and power supplies are where cold room projects tend to overrun, and Be Cool names both up front.
It also covers what happens after handover. The company offers 24/7 callouts and says it aims to attend cold room breakdowns within two to four hours, alongside maintenance contracts with priority response.
What to consider
Be Cool does not publish refrigeration or maintenance rates, so you will need quotes to compare it with a firm like Kept Cold. Its homepage shows a 5.0 Google rating, but the pages we reviewed did not show the number of reviews. The cold room FAQ gives a standard install time as “23 days”, which looks like a typo; confirm the timeline in writing.
Best fit
Restaurants, hotels and food producers planning a new or replacement cold room who want the same contractor for servicing and emergency cover afterwards, especially if they also need air conditioning work.
2. Kept Cold | Best for multi-site operators who want published maintenance prices
Overview
Kept Cold Ltd is a London commercial refrigeration repair and maintenance company with a City Road, EC1 address, and it says it works only on refrigeration, with no air conditioning or heating . It services cold rooms, display fridges, undercounter units, blast chillers, ice machines and prep counters across London within the M25.
Kept Cold publishes more of its terms than any other company here. Planned preventive maintenance starts at £60 per unit plus VAT, cold rooms from £120 plus VAT, out-of-hours labour is charged at 1.5 times the standard rate, and repairs carry a six-month parts and labour guarantee. It also says it is an authorised Foster Refrigeration partner, supplying new Foster units with installation and old-unit removal.
Key details
- Core offering: breakdown repair, planned maintenance, Foster equipment supply and installation.
- Coverage: London within the M25, with a focus on Central, North, East and West London.
- Customer fit: restaurants, hotels, dark kitchens, FM companies and groups with three or more sites.
- Pricing and terms: PPM from £60 per unit + VAT; cold rooms from £120 + VAT; ice machine cleans priced separately; out-of-hours labour at 1.5x.
Where Kept Cold stands out
Published prices make budgeting simpler. A kitchen with eight standalone units can estimate a PPM visit from the listed rate before calling, which none of the other six allow.
Its multi-site terms are specific. Kept Cold lists a two-hour emergency response target, four to six hour same-day attendance, a quarterly PPM calendar, 30-day consolidated invoicing and RAMS documentation for accounts with three or more sites. For an FM manager, that is close to a ready-made SLA.
What to consider
Being refrigeration-only means you will need a separate contractor for air conditioning. The homepage describes cold room repair and PPM, and Foster unit supply, but not the design and build of new cold rooms, so ask before assuming it can deliver a full installation. Response times are targets, not guarantees.
Best fit
Facilities managers and restaurant groups who want predictable maintenance costs and contractual response targets across several London sites.
3. Xpress Refrigeration | Best for quick-service restaurants that need fast reactive repairs
Overview
Xpress Refrigeration Ltd is a commercial refrigeration repair, servicing and installation company that says it was founded in 2005 and works across Central London, Canary Wharf, the M25 area and the South East . It covers fridges, freezers, cold rooms, multidecks, makelines, deli counters, ice machines, cellar cooling and gelato freezers, and also installs air conditioning.
The company names Costa, Subway, Domino’s and Pret a Manger as clients; we did not verify these relationships. Its homepage review widget showed a Google rating of 4.8 from 293 reviews when we checked on 7 October 2026.
Key details
- Core offering: reactive repair, servicing and installation of commercial refrigeration, including cold rooms and cellar cooling.
- Coverage: London and the South East.
- Customer fit: quick-service restaurants, cafés, pubs, convenience stores and gelato shops.
- Pricing and terms: not publicly listed; free survey and quote for installations; phone lines open 10:00 to 22:00 daily with a separate out-of-hours number.
Where Xpress Refrigeration stands out
It is set up for same-day fixes. Xpress says engineers arrive with spare parts on board and aim to finish work the same day, and many recent Google reviewers describe attendance within one to three hours, including weekends.
It knows fast-food kit. Makelines and pizza prep counters appear as their own service line, which suits chains and franchisees whose main risk is a prep counter failing mid-service.
What to consider
The same review feed includes several recent complaints about repeat faults after paid repairs and about after-sales support, including one on a walk-in freezer conversion. Get the repair guarantee and scope in writing before work starts. Prices are not published.
Best fit
Quick-service and café operators across London and the South East who mainly need fast reactive repairs on counters, display units and walk-ins.
4. RSI Professional | Best for warehouses and production sites
Overview
RSI Professional Ltd is an air conditioning, refrigeration and ventilation contractor based in Finchley, N3, which says it holds full Refcom certification and has more than 16 years of industry experience. It splits its refrigeration work into commercial (retail, hospitality and food service) and industrial (warehouses, storage, manufacturing and production).
Equipment covered includes blast chillers, cellar cooling, catering fridges, bespoke cold rooms and large walk-in freezer rooms. The company also publishes guidance on natural refrigerants such as CO₂ and ammonia for warehouse systems.
Key details
- Core offering: commercial and industrial refrigeration installation, commissioning, planned maintenance and repair.
- Coverage: London, with fast-response repairs offered within a 50km radius.
- Customer fit: warehouses, distribution centres, food production, retailers and hospitality venues.
- Pricing and terms: not publicly listed; free site survey; the company says you will never pay more than the quoted price.
Where RSI Professional stands out
Scale is the clearest difference. RSI describes new large cold room installations and commissioning for industrial units, which most kitchen-focused firms on this list do not.
Its maintenance scope is itemised. The page lists cold room diagnostics, safety checks, equipment testing, chemical cleaning, and filter, drain and condensate pump cleaning, and suggests servicing every three to six months. That gives buyers a checklist to compare against other quotes.
What to consider
The page shows a mobile number and a Gmail address, and no named clients or case studies. Larger buyers should ask for references, insurance certificates and Refcom registration details before shortlisting.
Best fit
Warehouse, distribution and production sites in and around London that need large cold or freezer rooms installed and serviced.
5. NTS Cooling | Best for labs and retailers needing specialist or display equipment in West London
Overview
NTS Cooling is a refrigeration and air conditioning company with a head office on Uxbridge Road, Ealing, W5, and further offices listed in Gerrards Cross. It supplies, installs and repairs cold rooms, display cabinets, multideck chillers, ice machines, bottle coolers, serve-over counters, and commercial fridges and freezers across London and surrounding counties.
Its brand list includes Hoshizaki, Scotsman, Williams, Arneg, Foster and Gram, and its site menu adds ultra-low temperature freezers, blast chillers, climatic test chambers and an equipment finance page. That range reaches beyond food service into scientific and testing applications.
Key details
- Core offering: equipment supply plus installation, maintenance and 24/7 emergency repair.
- Coverage: Central, West, North, East and South London and surrounding counties, from an Ealing base.
- Customer fit: restaurants, supermarkets, hotels, commercial kitchens, and labs needing low-temperature storage.
- Pricing and terms: not publicly listed; free quotes; a finance option is advertised; phone lines seven days a week.
Where NTS Cooling stands out
Specialist equipment is the main reason to shortlist it. Ultra-low temperature freezers and climatic test chambers are niche products, and few London refrigeration contractors list them alongside kitchen equipment.
It can supply as well as fit. For a retailer replacing multideck chillers or serve-over counters, having one firm source brands such as Arneg or Gram and then install them reduces handovers between supplier and engineer.
What to consider
NTS states its experience differently on the same page, citing both “30 Years’ Expertise” and “25+ Years’ Experience”; ask which entity and date the claim refers to. The site also lists catering equipment and property renovation services, so confirm that refrigeration engineers, not general trades, will attend your job.
Best fit
West London and Buckinghamshire businesses that need display or specialist low-temperature equipment supplied and installed by the same firm.
6. ACL London | Best for shops and bars that want a no-fee diagnostic visit
Overview
ACL London is a trading name of ACL Refrigeration & AC Ltd (Company No. 16021830), listed at Kemp House, City Road, EC1, and it works on both air conditioning and commercial refrigeration. It supplies and installs refrigerated display cabinets, cold and freezer rooms, counters, ice machines, storage cabinets, bottle coolers, blast freezers and chillers, and cellar coolers.
ACL says it is Refcom and ACRIB certified and that its engineers have more than 14 years of experience. It names Danfoss, Hoshizaki, Polar, Williams, Foster and Arneg among the brands it installs, and says it services equipment for customers ranging from supermarkets to small shops.
Key details
- Core offering: commercial and industrial refrigeration supply, installation, maintenance and repair, plus air conditioning.
- Coverage: named areas across Central, West, East, North and South London.
- Customer fit: independent retailers, bars, restaurants and supermarkets.
- Pricing and terms: refrigeration service and maintenance charges available by email; free call-out for contract and non-contract customers.
Where ACL London stands out
The free call-out is the clearest cost advantage on this list. For a corner shop with a failing bottle cooler, removing the call-out fee lowers the cost of finding out whether a repair is worth doing.
It also covers cellar cooling in depth. ACL’s site carries a long cellar cooling guide with indicative split-system installed costs of £2,300 to £6,000, which helps bars and wine retailers budget before a survey.
What to consider
Refrigeration rates are not on the site, so ask for them before booking. The “14+ years” figure describes engineers’ experience rather than the company’s own trading history. We found little project or client evidence on the page reviewed.
Best fit
Independent shops, bars and small food retailers who want a diagnostic visit without a call-out charge, and possibly AC from the same firm.
7. Premium Refrigeration | Best for small West and Central London kitchens needing repairs only
Overview
Premium Refrigeration is a repair and maintenance specialist based at Saltram Crescent, W9, which serves London areas including Chelsea, Westminster, Hampstead and Twickenham. Its commercial work covers walk-in coolers, display units, cold room repair and freezer room repair, from faulty thermostats to compressor failures.
It also repairs high-end domestic and US-style brands such as Amana, Maytag and Sub-Zero. The company states it has more than 35 years of experience, is F-Gas registered, and offers a company guarantee on its work.
Key details
- Core offering: commercial fridge, cold room and freezer room repair and maintenance.
- Coverage: London, with named areas in West and Central London.
- Customer fit: small restaurants, cafés, bars and premises with premium domestic-style refrigeration.
- Pricing and terms: not publicly listed, though the company describes its rates as transparent; open 24 hours, seven days.
Where Premium Refrigeration stands out
Its focus is narrow. Premium Refrigeration presents itself as a repair business rather than an installer, which can suit an operator who already has equipment and simply needs a breakdown fixed out of hours.
The brand overlap is unusual. Few commercial engineers also list Sub-Zero and Amana repairs, which helps boutique hotels, private members’ clubs or offices running domestic-style units next to commercial kit.
What to consider
New cold room installation is not described, so this is not the firm for a fit-out. The public information is thin: we found no client names, case studies or company registration number on the page reviewed, and its review link points to Yell rather than Google.
Best fit
Small kitchens and venues in West and Central London that need a 24-hour repair contact for existing fridges, cold rooms or freezer rooms.
How to choose a commercial refrigeration company in London
The biggest split on this list is between firms that design and build new cold rooms and firms that mainly repair existing equipment. Decide which you need first, then check the following before you sign anything.
- Check credentials on the registers. Ask for the company’s F-Gas certificate number and Refcom registration and look them up yourself, rather than relying on a logo on a website.
- Get the call-out and out-of-hours rates in writing. Only Kept Cold publishes its out-of-hours multiplier and only ACL London advertises a free call-out; everyone else quotes on request.
- Ask what the response time actually means. “Two to four hours” is usually a target for attendance, not a promise of repair. Ask what happens if parts are not on the van.
- Confirm the repair guarantee. Kept Cold states six months on parts and labour. For others, ask how long a repair is covered and whether a return visit for the same fault is charged.
- For a new cold room, confirm the site survey scope. It should cover floor insulation, drainage and a dedicated electrical supply, as Be Cool Refrigeration’s process describes. Ask whether an integral or remote condensing unit suits your kitchen.
- Ask for references for jobs like yours. A firm that repairs undercounter fridges daily may not have built a freezer room for a production site.
Frequently asked questions
How often should commercial refrigeration be serviced?
RSI Professional suggests every three to six months, and Kept Cold schedules multi-site PPM quarterly. The right interval depends on the equipment, how hard it works and how dirty the environment is; a busy kitchen’s condenser coils clog faster than a shop’s.
How much does commercial refrigeration maintenance cost in London?
Few companies publish prices. Kept Cold lists PPM from £60 per unit plus VAT and cold rooms from £120 plus VAT, checked 7 October 2026. Use that as a reference point when asking others for quotes, and compare like for like on what each visit includes.
How long does a cold room installation take?
RSI Professional says most standard installations take a few days, with larger rooms taking longer. Be Cool Refrigeration says larger or more complex builds can take up to a week. Lead times for panels and condensing units are separate, so ask about delivery as well as fitting time.
What is the difference between an integral and a remote cold room unit?
An integral unit sits on the cold room itself and is simpler and usually cheaper. A remote unit sits outside the building, which reduces noise and heat in the kitchen. Be Cool Refrigeration describes this choice on its cold room page; most installers will advise on it during the survey.
The bottom line
For a London food business planning a new cold room and wanting one contractor for installation, maintenance and emergency cover afterwards, Be Cool Refrigeration is our featured pick. If you run several sites and want published prices and SLA-style terms, Kept Cold is the stronger fit. Warehouses should talk to RSI Professional, labs to NTS Cooling, and smaller venues that just need a repair can compare Xpress Refrigeration, ACL London and Premium Refrigeration. Whichever you choose, get at least two quotes and check credentials on the public registers.
Part 2: Publishing fields
| Field | Suggestion |
| SEO title | 7 Best Commercial Refrigeration Companies in London (2026) |
| Meta description | Compare 7 London commercial refrigeration companies for cold rooms, repairs and maintenance, with pricing, coverage and who each one suits. |
| URL slug | /best-commercial-refrigeration-companies-london |
No author bio, expert reviewer, publication date or update history has been added; the publisher should supply these.
Part 3: Editor notes (not for publication)
Status: Blocked pending verification. The draft is complete, but six of seven competitors rest on one source page each, no credentials were checked against public registers, and Be Cool’s entity history needs confirming. Details below.
| Company | Review words (approx.) | Sources opened | Evidence type | Unresolved gaps |
| Be Cool Refrigeration | ~400 (may sit above the 15% band; trim if needed) | homepage, cold room page | Company website only | Google review count; Refcom/F-Gas register entries; “23 days” install typo; “Est. 2004” vs Company No. 13901261, whose number range suggests a much more recent incorporation (not verified) |
| Kept Cold | ~370 | homepage | Company website | Second source; whether it builds new cold rooms; Foster partner status not confirmed with Foster |
| Xpress Refrigeration | ~320 | homepage | Company website plus Google reviews shown in its widget | Second source; named clients (Costa, Subway, Domino’s, Pret) unverified; review figure taken from its own widget, not Google directly |
| RSI Professional | ~320 | refrigeration page | Company website | Second source; Refcom certification; no clients or case studies |
| NTS Cooling | ~340 | commercial refrigeration page | Company website | Second source; conflicting experience claims (30 years / 25+ years; a search snippet of its cold room page also says “since 2002”) |
| ACL London | ~320 | refrigeration page | Company website | Second source; Refcom/ACRIB status; refrigeration rates |
| Premium Refrigeration | ~320 | homepage | Company website | Thinnest evidence on the list; no company number, clients or reviews checked |
Disclosure requiring approval: “This is a sponsored article. Be Cool Refrigeration paid for this placement and appears first as our featured pick. No other company on this list paid to be included, was contacted, or reviewed this article before publication.” Replace with the publisher’s house wording if it has one, and confirm the publisher name.
Material assumptions
- Topic set to commercial refrigeration (not AC), target reader a London food or hospitality business, seven companies, UK English, no call to action (none was supplied).
- Publisher relationship taken as paid guest-post placement.
- Cool-Tec was excluded despite a London refrigeration page because it is based in Wareham, Dorset; Debonair Cooling was dropped because its refrigeration page returned a 404; London Refrigeration’s site would not load.
- Ranking after position 1 is editorial judgement on scope match and published detail, stated as such in the methodology.
Supplied or company claims excluded or softened
- Be Cool’s “Rated 5/5 by London businesses”, “Trusted by 500+ businesses”, “2,000+ projects” and brand-logo clients (other than the two named project pages) were not used because they could not be verified.
- Be Cool’s O2 Arena reference was left out; only a van photo caption supports it.
- Be Cool’s site testimonials were not quoted; they are company-selected.
To clear the block: look up each company on the Refcom and F-Gas registers, confirm Be Cool’s legal entity and trading history with the client, get Be Cool’s Google review count, and add one independent source per competitor (Companies House, a trade body listing, or a review platform).

Introduction
The AI music generation has become surprisingly affordable. What used to cost hundreds of dollars in a recording studio can now be produced for less than a nickel per track — if you know which platform to subscribe to. But published "monthly prices" rarely tell the full story. A $9.99 plan with 1,000 credits isn't necessarily cheaper than a $23.99 plan with 10,000 credits, and annual discounts can cut per-song costs by up to 50%.
This article breaks down the ten most cost-effective AI music generator platforms available right now, calculated by the real metric that matters: actual dollar cost per song generated. We factored in subscription price, monthly credit allowance, credit-to-song conversion ratios, and annual billing discounts to produce an apples-to-apples comparison.
How We Test
To rank these platforms fairly on cost, we used the following criteria:
Per-song cost (annual billing): The effective price of generating one song under the cheapest subscription tier available, calculated using the platform's own credit conversion rules.
- Per-song cost (monthly billing): The same metric calculated at standard monthly pricing, without annual discounts.
- Entry tier affordability: The lowest paid plan's monthly cost and what you actually get for it.
- Free tier value: How much you can generate before paying anything.
- Hidden costs or caps: Download limits, concurrent generation restrictions, and credit rollover rules that affect real usage economics.
- All numbers below come directly from each platform's public pricing pages.
TL;DR Comparison Table
| Rank | Platform | Cheapest Per-Song Cost | Entry Paid Plan | Free Tier |
|---|---|---|---|---|
| 1 | musicgenerator | ~$0.034/song (Ultra annual) | $7.9/mo (Starter annual) | 6 signup credits |
| 2 | AIMusic | $0.012/song (Ultra) | $7.99/mo (Pro annual) | 15 credits/day |
| 3 | Brev AI | $0.012/song (Ultra) | $7.99/mo (Pro annual) | 25 credits/day |
| 4 | Nafy AI | $0.021/song (Pro annual) | $12.42/mo (Basic annual) | 1.5 gens/day |
| 5 | Udio | ~$0.017/gen (Pro annual) | $8/mo (Standard annual) | 10 credits/day |
| 6 | AI Song Maker | $0.035/song (Pro annual) | $10.49/mo (Basic annual) | 20 credits/day |
| 7 | aisong.io | $0.025/song (Premium) | $9.99/mo (Starter) | 10 credits/day |
| 8 | MelodyCraft | $0.043/song (Premium annual) | $16/mo (Pro annual) | 3-day trial |
| 9 | Tad AI | ~$0.06/gen (Pro) | $7.99/mo (Standard) | 21 signup credits |
| 10 | Mubert | $0.0625/gen (Ultra annual) | $11.67/mo (Creator annual) | 25 gens/month |
The 10 Cheapest AI Music Generators
1. musicgenerator
musicgenerator is a one-stop online AI audio platform that balances generation cost with feature breadth. It operates on a tiered model system where the Luna model (m-luna) is accessible across all plans, while the Terra (m-terra) and Sol (m-sol) models unlock at the Plus tier and above for more expressive output. Beyond music generation, the platform bundles supporting tools like a song lyrics generator, AI Song Cover Generator, stem splitter, and vocal remover — all accessible from the same credit pool, so you don't pay separately for auxiliary features.
- Features:
- Three AI audio models: m-luna (all plans), m-terra and m-sol (Plus+)
- AI music generation from text prompts or custom lyrics
- Stem splitting, vocal remover, and song extension tools
- Reference audio upload (Plus and Ultra plans)
- Licensed audio upload for remixing (Ultra only)
- AI Singing Voice Generator and Personas (Ultra only)
- Pricing (annual billing):
- Free: $0 — 6 one-time signup credits, online preview only
- Starter: $7.9/mo — 180 credits/mo, MP3 download
- Plus: $16.9/mo — 500 credits/mo, lossless WAV, commercial license
- Ultra: $69.9/mo — 2,300 credits/mo, all models, licensed audio upload
Each generation consumes 3 credits, meaning the effective per-generation cost ranges from about $0.13 on Starter to $0.09 on Ultra when billed annually.
- Pros:
- Credit packs never expire (available Starter Pack through Enterprise Pack)
- Clear model tiering makes it easy to pick a plan that matches your needs
- Supports reference audio upload for style guidance on Plus+
- Cons:
- Free tier credits are one-time, not recurring
- No download on the free plan — only in-browser preview
Best for: Creators who want flexible scaling — start with Starter for MP3 output, upgrade to Plus when commercial licensing and lossless WAV become necessary.
2. AIMusic (aimusic.so)
AIMusic runs a credit-based system with per-feature pricing that rewards users who do more than just generate full songs — vocal removal, music extension, and cover art each have their own credit costs.
- Features:
- V6 mini (all plans), V6 (Pro+), V6 Wild (Ultra only)
- Song generation: 5 credits/song
- Music extension: 3 credits per operation
- Vocal removal: 5 credits per file
- AI cover image: 2 credits; sound effects: 1 credit
- Lyrics generator and lyrics video (free on Pro+)
- Pricing:
- Free: 15 credits/day refresh (3 songs/day), 7-day storage, no download
- Pro (annual): $7.99/mo, 1,500 credits/mo, 4 concurrent tasks
- Ultra (annual): $23.99/mo, 10,000 credits/mo, 10 concurrent tasks, lossless WAV
- Per-song cost:
- Pro: $0.0266/song (about 2.66 cents)
- Ultra: $0.0120/song (about 1.20 cents)
- Pros:
- Among the cheapest per-song cost on Ultra tier
- Granular credit pricing means you only pay for what you use
- Commercial license certificate available on annual plans
- Cons:
- Free tier generations are public and limited to 7-day storage
- Credits don't roll over month-to-month
- Best for: High-volume creators who need predictable bulk pricing and only generate full songs occasionally.
3. Brev AI (brev.ai)
Brev AI uses nearly identical pricing to AIMusic, with V6 mini, V6, and V6 Wild models tiered across plans. The per-feature credit system is also the same: 5 credits per song, 3 for extensions, 2 for cover art, 1 for sound effects.
- Features:
- Three-tier model system (V6 mini / V6 / V6 Wild)
- Song generation from text or custom lyrics
- Vocal remover and stem splitter (Ultra adds stem splitting for self-generated tracks)
- Music extension and AI cover image generation
- Lyrics video (free on paid plans)
- Unlimited cloud storage on Pro and Ultra
- Pricing:
- Free: 25 credits/day (5 songs/day), 7-day storage, public generations
- Pro (annual): $7.99/mo, 1,500 credits/mo
- Ultra (annual): $23.99/mo, 10,000 credits/mo, lossless WAV
- Per-song cost:
- Pro: $0.0266/song
- Ultra: $0.0120/song
- Pros:
- Generous free tier at 25 daily credits
- Ultra tier matches AIMusic for lowest per-song cost
- PDF commercial license certificate on annual subscriptions
- Cons:
- Monthly credits don't roll over
- Pro tier limited to MP3 — WAV is Ultra-exclusive
- Best for: Hobbyists exploring AI music who want 5 free songs daily before committing to a paid plan.
4. Nafy AI
Nafy AI prices by "generations" rather than credits, with one generation producing two song variants. This makes its per-song math straightforward: half the per-generation price.
- Features:
- V6, V5.5, and V5 model selection across all tiers
- AI Music Extension and AI Music Editor (segment-level editing)
- AI Song Cover Generator with cross-genre reconstruction
- Vocal remover and custom voice training (Voice Changer)
- AI Singing Video Generator for lip-sync videos
- Lossless WAV and MIDI export on paid plans
- Pricing (annual):
- Free: 1.5 generations/day (3 songs/day), 14-day storage, no commercial use
- Basic: $12.42/mo, 125 gens/mo (250 songs)
- Standard: $24.92/mo, 500 gens/mo (1,000 songs), 4 concurrent
- Pro: $49.92/mo, 1,200 gens/mo (2,400 songs), 8 concurrent
- Per-song cost:
- Basic: $0.0497/song
- Standard: $0.0249/song
- Pro: $0.0208/song
- Pros:
- Pay-as-you-go credits never expire and unlock most Pro features
- MIDI export supported on paid tiers — rare among competitors
- Each generation yields 2 variants for one price
- Cons:
- Higher entry price ($12.42/mo) than AIMusic or Brev AI
- Free tier excludes commercial use and downloads
- Best for: Producers who want MIDI output for further DAW editing and value getting two takes per prompt.
5. Udio
Udio takes a different approach by charging primarily by generation count rather than per song. A single generation produces 2 songs (4 in the free tier's batch), and each full-length (130-second) track consumes credits proportionally.
- Features:
- 32-second clips or full 130-second (2:10) songs
- Remix and Extend existing tracks
- Precise music and lyrics editing
- Style Reference, Blend Styles, and Reduce Styles controls
- Voice Control with library of voices plus custom voice saving
- Audio upload for creative guidance
- Pricing:
- Free: 10 credits/day, 100/mo, 3 full-length songs daily cap
- Standard: 8/moannual(10 monthly), 2,400 credits/mo, 6 parallel
- Pro: 24/moannual(30 monthly), 6,000 credits/mo, 10 parallel
- Credit cost:
- Standard annual: $0.00333/credit
- Pro annual: $0.00400/credit
- Add-on packs: $3/100 credits or $25/1,000 credits
- Pros:
- Lowest per-credit cost in this comparison on Standard annual
- Strong control features like style blending and voice reuse
- Student discounts available on Pro
- Cons:
- Monthly credits don't roll over
- Shorter maximum song length (130 seconds) than many competitors
- Best for: Experimental producers who prioritize style control and voice consistency over long-form output.
6. AI Song Maker (aisongmaker.io)
AI Song Maker operates on a 5-credits-per-song model with one of the most generous credit rollover policies in the industry — unused subscription credits roll to the next month, up to 3× your monthly allocation.
- Features:
- Text/Lyrics to Music with harmony and melody
- AI Song Cover Generator with style reconstruction
- Extend Song and Upload Custom Music (2–8 min uploads on paid)
- Custom Voice Model training (AISinger)
- VibeSeed — uses your song as a mood seed
- AI Music Video Generator (10 sec to 5 min visuals)
- AI Singing Photo Generator for lip-sync videos
- Pricing (annual):
- Free: 20 credits/day (4 songs/day), 30-day storage, non-commercial
- Basic: $10.49/mo, 12,000 credits/year
- Standard: $20.99/mo, 30,000 credits/year, 10 concurrent
- Pro: $41.99/mo, 72,000 credits/year, unlimited concurrent
- Per-song cost:
- Basic: $0.0525/song
- Standard: $0.042/song
- Pro: $0.035/song
- Pros:
- Credits roll over month-to-month (3× cap)
- Unique features like VibeSeed and AISinger voice training
- Downloadable commercial license certificate with unique ID per song
- Cons:
- Credit packs ($6/400 or $100/10,000) cost more per credit than the subscription
- Free tier requires attribution
- Best for: Creators with uneven monthly workloads who need credits to carry forward.
7. aisong.io
aisong.io offers a flat 10-credits-per-generation rate, with each generation producing 2 songs. Commercial licensing is included on every plan — including the free tier.
- Features:
- Text to Song, AI Song Edit, AI Rap generation
- Extend, Cover, and segment replacement
- Stem Splitter and LRC lyrics generator
- Lyrics card maker and AI sound effects
- Free unlimited tools: BPM calculator, audio-to-text, MP3 converter, audio trimmer
- AI music video and lip-sync video generators
- Pricing:
- Free: 10 credits/day (new users get 20/day for first 15 days), 7-day storage
- Starter: $9.99/mo (reg. $14.99), 1,000 credits/mo (~200 songs)
- Standard: $19.99/mo (reg. $29.99), 3,300 credits/mo (~660 songs)
- Premium: $39.99/mo (reg. $59.99), 7,900 credits/mo (~1,580 songs)
- Per-song cost:
- Starter: $0.050/song
- Standard: $0.030/song
- Premium: $0.025/song
- Pros:
- Commercial license included even on free plan
- Free bundled utilities (BPM, converters) consume zero credits
- New-user bonus doubles free credits for 15 days
- Cons:
- Credits reset each billing cycle — no rollover
- Discounted prices listed may be promotional
- Best for: Users who want commercial rights from day one without paying for a subscription.
8. MelodyCraft
MelodyCraft positions itself at a higher price point but compensates with aggressive 50% annual discounts and extensive premium features like API access and white-label options.
- Features:
- Text to Song and Lyrics to Music generation
- AI Lyrics Generator and AI Song Cover Generator
- Vocal Removal Tool and Song Extension (up to 10 min on Pro, unlimited on Premium)
- 5 concurrent generations (Pro) or 10 (Premium)
- API access, white-label options, custom AI model training (Premium only)
- AI photo, video, voice, and story generators included
- Pricing:
- Pro: 32/mo(16/mo annual), 1,000 credits/mo (~200 songs), 3-day trial
- Premium: 52/mo(26/mo annual), 3,000 credits/mo (~600 songs), 7-day trial
- Per-song cost (5 credits/song):
- Pro monthly: $0.160/song | Pro annual: $0.080/song
- Premium monthly: $0.087/song | Premium annual: $0.043/song
- Pros:
- 50% annual discount — largest in this ranking
- 14-day money-back guarantee
- Enterprise-grade features (API, white-label) on Premium
- Cons:
- No perpetual free tier — only trial periods
- Monthly billing is expensive compared to competitors
- Best for: Agencies and businesses who can commit to annual billing and need API or white-label capabilities.
9. Tad AI
Tad AI uses a slider-based credit system that lets Standard and Pro users pick their monthly credit allowance (500–1,500 for Standard, 2,000–4,000 for Pro).
- Features:
- Tad 6.0 AI audio engine with Smart and Custom modes
- AI Music, Rap, Cover, and Phonk generators
- Vocal Remover and Stem Splitter (Standard+)
- AI Music Video Generator
- Reference audio upload — includes pasting TikTok, Instagram, Facebook links
- AI Lyrics enhancement (polish, expand, trim)
- Custom singer voice model training
- Pricing:
- Free: 21 one-time signup credits, standard voice models
- Standard: $7.99/mo, 500–1,500 credits/mo, 3 concurrent
- Pro: $23.99/mo, 2,000–4,000 credits/mo, 6 concurrent
- Per-credit cost:
- Standard: $0.016/credit
- Pro: $0.012/credit
- Pros:
- Unique ability to paste social media audio URLs as references
- Slider-based credit customization
- 20% annual discount available
- Cons:
- Published materials don't specify a fixed per-song credit cost
- No permanent free tier — only one-time signup credits
- Best for: TikTok and Instagram creators who want to generate music inspired by viral social audio.
10. Mubert
Mubert specializes in royalty-free background music for creators, with a hard commercial-use boundary: music generated here cannot be released to Spotify, Apple Music, or registered with Content ID regardless of plan.
- Features:
- Chat2Music AI v2 (paid unlocks full version)
- Text 2 Music, Image 2 Music, MusicGen AI
- Full Track Editor: modify structure, regenerate sections, edit stems, Quick Remix, adjust BPM and key
- Up to 60-minute track generation on Ultra
- Copyright Checker included on all plans
- 30-day Plus/Max trial of Fuse (video) and Cast (podcast) tools on Pro and Ultra
- Pricing (annual):
- Free: $0, 25 generations/mo, 30-min daily cap, watermark + attribution
- Creator: $11.67/mo, 100 gens/mo, 10-min max tracks
- Pro: $32.49/mo, 500 gens/mo, 25-min tracks, unlimited downloads
- Ultra: $62.50/mo, 1,000 gens/mo, 60-min tracks, full agency rights
- Per-generation cost (annual):
- Creator: $0.117/gen
- Pro: $0.065/gen
- Ultra: $0.0625/gen
- Pros:
- Longest track duration available (60 min on Ultra)
- Full Track Editor offers rare structural control
- Bundled Copyright Checker on every plan
- Cons:
- Highest per-generation cost on Ultra in this list
- Streaming platform release prohibited on all plans
- Best for: Video producers and podcasters needing long-form background music with no Spotify-style ambitions.
Key Takeaways
Lowest per-song cost overall: AIMusic Ultra and Brev AI Ultra both land at $0.012/song, making them the mathematical winners for pure volume.
- Best entry-tier value: AIMusic Pro and Brev AI Pro at $7.99/mo annual both hit $0.0266/song — strong budget picks.
- Biggest annual discount: MelodyCraft's 50% off annual pricing cuts Premium from $52 to $26/mo.
- Best free tier: Brev AI's 25 daily credits (5 songs/day) narrowly beats AIMusic's 15 daily credits.
- Longest tracks for the money: Mubert Ultra delivers 60-minute tracks that most competitors can't match at any price.
Credits that don't vanish: AI Song Maker's rollover policy (up to 3× monthly allocation) and Nafy AI's permanent pay-as-you-go packs stand out from rivals that reset monthly.
Conclusion
Per-song cost alone isn't the full picture. A $0.012/song rate means nothing if the platform doesn't support the song length, licensing terms, or editing tools you need. The cheapest platforms in this list — AIMusic and Brev AI — reward high-volume users on their top tiers, while Udio and Nafy AI offer better value for creators who want advanced control features. Mubert costs more per generation but delivers track lengths no competitor matches. Before subscribing, check how each platform handles credit rollover, download formats, and commercial licensing — those three factors often matter more than headline price.

Efficiency in a wastewater treatment system isn’t just about “shrinking” the treatment unit into a shipping container. Efficient system operation occurs when each treatment stage has a well-defined purpose, upstream processes safeguard downstream equipment, controls are responsive to the operating conditions, and the final treatment level is commensurate with the desired effluent quality.
The practical concept of containerized wastewater treatment systems is one of these. Rather than focus on the benefits of the container, the more effective design is to consider the container as an engineered platform to coordinate biological, physical-chemical, membrane, pumping, dosing and control functions.
QILEE uses this method for industrial wastewater, municipal sewage, decentralized treatment and water-reuse projects. The containerized configurations of the wastewater treatment process can include biological treatment, dissolved air flotation (DAF), chemical dosing, membrane bioreactor technology, filtration, nanofiltration (NF), reverse osmosis (RO), and other supporting equipment depending on wastewater characteristics.
This does not mean that there is one standard process for each site. Efficiency is achieved by only using the treatment functions needed by the wastewater.
Why QILEE Containerized Wastewater Treatment Systems Can Operate Efficiently
To make a containerized plant efficient, process design, equipment placement and controls should be considered as an integrated system and not as individual parts of the system.
In wastewater projects, this is important because each phase is dependent on the previous phase. If solids are not removed properly, the fouling of membranes may be greater. Chemical dosing, which is not stable, can have a negative effect on separation performance. Biological loading may be incorrect and impact the quality of water in the downstream environment. For these interactions, it is possible to think about them in advance in an integrated design.
Process Selection Starts With the Wastewater, Not the Equipment
Industrial wastes generate various treatment issues. Food-processing wastewater may contain significant amounts of biodegradable organic matter, while metal finishing wastewater may need specific removal of metals. Oily wastewater requires a different pretreatment from municipal sewage, and high-ammonia wastewater may require a special removal stage.
Therefore, the first step to efficient wastewater management is wastewater characterization. The treatment train may be affected by flow rate, pH, suspended solids, COD, ammonia nitrogen, oil, salt, metals, and the required standard of discharge or reuse.
Below is a helpful chart of the impact of common processes.
| Process | Primary Role | Efficiency Contribution |
| Combining DAF and chemical dosing | Removes suspended solids, oils, flocs or specific contaminants | Reduces the load on downstream processes |
| The water quality treatment process is biological treatment using the AO/A²O process. | Helps remove biodegradable pollutants and treat nutrients | Applies organic and nutrient loads in a biological manner |
| MBR / TMBR | Combined biotechnological treatment and membrane separation | Effective solid/liquid separation in small volume |
| Multimedia filtration | Removes suspended material from water. | Safeguards smaller downstream processes |
| NF | Selective membrane separation | Enhances more complex treatment as required to achieve greater separation |
| RO | Removes dissolved salts and other dissolved contaminants. | Aids in achieving higher levels of re-use or purified-water goals |
Pretreatment Protects the Processes That Follow
Long-term operating efficiency can often be won or lost in pretreatment. Excessive solids, oils or chemically removable contaminants are better managed prior to becoming a downstream burden by membranes and biological systems.
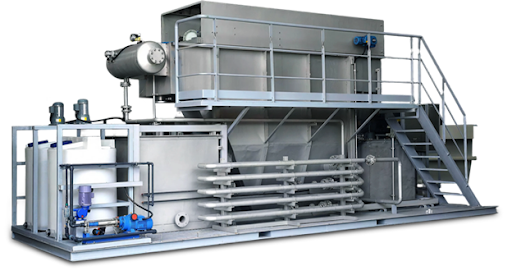
As part of its integrated product range, QILEE offers containerized physical-chemical configurations for combining chemical dosing, coagulation-flocculation, DAF, lamella clarification, neutralization, sedimentation, multimedia filtration, activated carbon filtration or chemical oxidation, depending on the application.
Oily or emulsified wastewater may require separation before biological or membrane treatment and heavy-metal wastewater may require chemical precipitation. The intent is to avoid usage of downstream processes to do work that can be done more effectively in a pretreatment process.
ALT text: QILEE containerized wastewater pretreatment system with chemical dosing, DAF, filtration, piping, and control equipment
MBR Integration Saves Space Without Eliminating Process Control
Membrane bioreactor technology can be useful in applications that demand both biological treatment and good solid-liquid separation in a small area.
An MBR system separates treated water from suspended biomass with the help of membranes while also breaking down biodegradable pollutants in the biological treatment process. This eliminates the need to rely on a traditional secondary clarifier for final separation of biomass.
The efficiency gain is hence not just a finer filtration but functional integration. Compact plant layouts and effluent separation are supported by MBR; however, much like other processes, membrane performance is dependent on suitable upstream conditions, aeration, cleaning, hydraulic loading, and maintenance.
Automated Controls Reduce Unnecessary Manual Intervention
Wastewater is not always steady-state. Normal operating conditions may include changes in flow, pollutant concentrations, tank levels, pressure, and chemical demand.
Integrated controls enable pumps, dosing systems, valves, alarms, and monitoring instruments to be switched on by the same control logic. Intelligent pump valves and smart control functions are available for QILEE’s containerized systems, with an integrated system range that also offers automated dosing systems and packaged control panels.
Automation does not render a wastewater system maintenance-free. There is still work to be done by operators for inspection, alarm response, cleaning, and treatment performance verification. Value is consistency: routine actions can be coordinated automatically, and abnormal conditions are easier to detect.
Compact Layout Can Improve Operation and Maintenance
A crowded container is not an efficient container. There should be sufficient space available to inspect, service the membrane, maintain pumps, calibrate instruments, and replace wear items.
Effective containerization of equipment, therefore, goes beyond the simple objective of maximizing equipment density. This will be affected when pipes are routed, valves can be accessed, drainage and ventilation can be done, the operator can move around, and clearances for services are considered.
Pre-integrating primary equipment also minimizes the number of interfaces that have to be put together on site. Much of the process coordination between the internal team has been completed, though there is remaining work in the following stages: foundations, external piping, and utility connections, and commissioning.
Treatment Depth Should Match the Final Water-Quality Target
One common way to increase energy use and operating expenses is to over-treat the water. The other problem, inadequate treatment, can lead to compliance or reuse problems.
Biological treatment and solid-liquid separation can be justified in a discharge application, and extra filtration, NF, or RO may be justified in a reuse project. If the water is highly dominated by ammonia nitrogen, a targeted deamination process may be necessary instead of the application of additional general filtration processes.
That is why the required effluent quality should be determined early. It helps to decide if advanced membrane treatment is required and avoid the inclusion of the equipment without putting a measurable treatment service.
Conclusion
The most efficient containerized wastewater treatment systems are not simply the most compact. Pretreatment eliminates pollutants, which will complicate subsequent treatment processes; biological processes treat biodegradable components; membranes offer controlled separation when necessary; and automatic controls coordinate normal operation.
QILEE can incorporate these capabilities into a containerized treatment package as dictated by the characteristics of the influent, required treatment capacity, site conditions and final water quality goals for industrial and decentralized projects.
This is how to judge a containerized plant: What is it doing, what is it protecting, and is it needed for the target effluent quality? Once the answers to those questions are obvious, the concept of compact design is no longer a stretch for space but rather a useful method to construct a cohesive treatment system.
The electronics industry continues to evolve rapidly, creating a growing demand for smaller, faster, and more efficient printed circuit boards. As electronic devices become increasingly sophisticated, manufacturers require advanced PCB technologies that support high component density, excellent signal integrity, and reliable performance. High-Density Interconnect (HDI) technology has emerged as an essential solution for meeting these requirements.
Choosing a reliable hdi pcb manufacturer is critical for businesses developing innovative electronic products. FastTurn PCBA offers advanced PCB manufacturing and assembly solutions designed to support complex circuit designs, compact electronic devices, and demanding industrial applications. With a focus on manufacturing precision, quality control, and efficient production processes, FastTurn PCBA helps businesses turn sophisticated circuit designs into functional electronic products.
Understanding HDI PCB Technology
High-Density Interconnect (HDI) printed circuit boards are advanced circuit boards designed to accommodate more electrical connections within a smaller physical area. Unlike conventional PCBs, HDI boards incorporate specialized manufacturing techniques, including microvias, fine lines, smaller spacing, and advanced multilayer structures.
These technologies allow engineers to create compact electronic systems without sacrificing essential functionality or electrical performance.
HDI PCBs commonly feature:
- Microvias: Small drilled holes that connect adjacent PCB layers and enable compact routing.
- Fine-Line Circuitry: Narrow traces and spacing that support high-density component placement.
- Multilayer Construction: Multiple conductive layers that accommodate complex circuit designs.
- Blind and Buried Vias: Specialized connections that improve routing flexibility while conserving board space.
- Advanced Materials: Carefully selected substrates that support electrical reliability and thermal performance.
- High Component Density: Efficient placement of electronic components within limited board dimensions.
These characteristics make HDI technology particularly valuable for modern electronic devices requiring miniaturization and advanced functionality.
Why Choose FastTurn PCBA as Your HDI PCB Manufacturer?
Selecting the right manufacturing partner significantly influences electronic product quality, development efficiency, and long-term reliability. FastTurn PCBA focuses on providing PCB manufacturing and assembly solutions that address the technical requirements of modern electronics.
Advanced PCB Manufacturing Capabilities
HDI PCB manufacturing requires precise production processes and specialized equipment. Hdi pcb manufacturer supports advanced circuit board solutions intended for applications where traditional PCB manufacturing techniques may not provide sufficient routing density.
Manufacturing considerations include fine-line patterning, accurate layer alignment, controlled drilling, and reliable interconnections between conductive layers.
These processes are essential for producing circuit boards that meet demanding electrical and mechanical requirements.
Support for Complex PCB Designs
Modern electronic products often contain powerful processors, communication modules, sensors, and other sophisticated components. Integrating these elements into compact devices requires careful PCB design and manufacturing coordination.
FastTurn PCBA helps customers address challenging PCB requirements through manufacturing-oriented solutions that support complex board structures and dense component layouts.
PCB Manufacturing and Assembly Solutions
Working with a provider that supports both PCB fabrication and assembly can simplify electronic product development.
FastTurn PCBA provides PCB manufacturing and assembly services that help businesses coordinate important production stages.
Potential advantages of integrated manufacturing and assembly include:
- Improved communication between fabrication and assembly teams.
- Reduced coordination requirements across multiple suppliers.
- Better alignment between PCB design and assembly requirements.
- More efficient prototype development.
- Simplified production planning.
- Improved consistency throughout manufacturing workflows.
This integrated approach can be particularly beneficial for businesses developing complex electronic products.
Key Benefits of HDI PCB Technology
HDI printed circuit boards offer several important advantages over conventional PCB structures. These benefits make them suitable for industries where compact designs and advanced electronic performance are essential.
Smaller and Lighter Electronic Devices
One of the most significant advantages of HDI technology is its ability to reduce PCB size while maintaining complex electrical functionality.
Microvias and fine-line routing allow designers to create dense interconnections without requiring excessive board space.
This capability is particularly useful for smartphones, wearable electronics, medical devices, and portable communication equipment.
Improved Signal Integrity
High-speed electronic systems require carefully designed signal paths to minimize interference and maintain stable communication between components.
HDI technology provides additional routing flexibility, allowing engineers to optimize signal paths and reduce unnecessary connection lengths.
When combined with appropriate impedance control and layout practices, these features can improve signal integrity in high-frequency and high-speed applications.
Enhanced Design Flexibility
Traditional PCB structures may limit the placement of components and the routing of complex electrical connections.
HDI technology provides engineers with more options for arranging components and connecting multiple circuit layers.
This flexibility supports innovative product designs and helps manufacturers address demanding space constraints.
Potential for Better Electrical Performance
HDI boards can provide shorter interconnection paths and more efficient routing structures.
These characteristics may reduce certain parasitic effects and improve electrical performance when supported by proper circuit design.
However, overall performance also depends on material selection, stack-up design, manufacturing accuracy, and component characteristics.
Support for Advanced Components
Modern electronic systems frequently incorporate fine-pitch ball grid arrays, miniature integrated circuits, and other densely packaged components.
HDI PCB technology helps accommodate these components by providing advanced routing capabilities beneath and around complex component footprints.
HDI PCB Manufacturing Process at FastTurn PCBA
Producing reliable HDI printed circuit boards involves several carefully controlled manufacturing stages. Each stage contributes to the electrical performance, mechanical integrity, and overall quality of the finished board.
Design Review and Engineering Preparation
The manufacturing process begins with evaluating the PCB design and determining whether it meets fabrication requirements.
Important considerations include:
- Board dimensions and layer count.
- Trace width and spacing.
- Microvia dimensions and placement.
- Material specifications.
- Layer stack-up configuration.
- Copper thickness requirements.
- Controlled impedance specifications.
- Component placement and assembly considerations.
A detailed design review helps identify potential manufacturing challenges before production begins.
Material Selection
Selecting appropriate PCB materials is essential for achieving reliable electrical and thermal performance.
HDI boards may require specialized laminates depending on operating frequency, environmental conditions, and product requirements.
Material selection influences dielectric properties, dimensional stability, thermal resistance, and overall manufacturing compatibility.
Laser Drilling and Microvia Formation
Microvias are among the defining features of HDI PCB technology.
Laser drilling is commonly used to create small, precise holes that connect selected conductive layers.
These holes are subsequently processed and metallized to establish electrical connections.
Accurate microvia formation is essential because poorly formed or unreliable interconnections can compromise board performance.
Layer Imaging and Circuit Formation
During this stage, conductive circuit patterns are formed on the PCB layers.
Advanced imaging and etching processes help create the fine traces and narrow spacing required for high-density designs.
Precise pattern formation is particularly important when manufacturing compact electronic boards with complex routing structures.
Layer Lamination
Multilayer HDI boards require accurate alignment and bonding of conductive and insulating layers.
Some advanced HDI structures involve sequential lamination cycles to create multiple levels of microvia interconnections.
Proper lamination helps maintain structural integrity and reliable electrical connections.
Inspection and Electrical Testing
Quality verification is an essential part of PCB manufacturing.
Depending on the board design and production requirements, inspection and testing may include automated optical inspection, electrical continuity testing, dimensional verification, and other appropriate quality checks.
These procedures help identify manufacturing defects before boards proceed to assembly or final delivery.
Applications of HDI PCBs Across Different Industries
HDI technology supports a wide range of industries that require advanced electronic systems, compact designs, and dependable electrical performance.
Consumer Electronics
Consumer electronics manufacturers continually seek smaller devices with greater processing power and improved functionality.
HDI PCBs are widely used in products such as:
- Smartphones and tablets.
- Smartwatches and wearable devices.
- Digital cameras.
- Portable gaming systems.
- Wireless communication devices.
- Compact computing equipment.
These products benefit from dense circuit layouts and efficient use of internal space.
Medical Electronics
Modern medical equipment frequently requires compact, sophisticated circuit boards capable of supporting accurate electronic functions.
HDI technology can be useful in portable diagnostic equipment, patient monitoring systems, wearable medical devices, and certain imaging technologies.
For medical applications, PCB manufacturing must also consider applicable regulatory requirements, traceability, risk management, and product-specific quality standards.
Automotive Electronics
Automotive technology increasingly relies on advanced electronic control systems, sensors, and communication networks.
HDI boards can support compact designs used in advanced driver assistance systems, infotainment equipment, communication modules, and other automotive electronics.
Automotive applications may require additional environmental testing and qualification depending on operating conditions.
Telecommunications
High-speed communication systems require carefully designed circuit boards capable of supporting complex signal routing.
HDI technology is useful in networking equipment, wireless communication systems, and compact telecommunications modules.
Proper impedance management and material selection are particularly important in these applications.
Industrial Automation
Industrial equipment increasingly incorporates sophisticated electronic control systems.
HDI PCBs can support compact controllers, sensor interfaces, monitoring equipment, and communication modules used in automated manufacturing environments.
HDI PCB vs. Traditional PCB: Understanding the Differences
Although conventional PCBs remain suitable for many electronic products, HDI technology provides additional capabilities for applications requiring high interconnection density.
| Feature | Traditional PCB | HDI PCB |
| Circuit Density | Generally lower | Higher |
| Via Technology | Primarily mechanically drilled vias | Microvias, blind vias, and buried vias |
| Trace Width and Spacing | Typically larger | Supports finer geometries |
| Component Placement | More limited in dense layouts | Better support for compact components |
| Manufacturing Complexity | Generally simpler | More advanced processes |
| Production Cost | Often lower for simple designs | May involve higher fabrication costs |
| Applications | General electronics | Compact and complex electronics |
The appropriate technology depends on product requirements, design complexity, manufacturing volume, and budget.
For applications that do not require high-density routing, conventional PCBs may provide a more economical solution.
However, HDI technology becomes increasingly valuable when space limitations and component complexity make traditional routing approaches impractical.
Important Factors When Selecting an HDI PCB Manufacturer
Choosing a dependable FastTurn PCBA requires more than comparing production prices. Businesses should evaluate technical capabilities, engineering support, quality practices, and production flexibility.
Manufacturing Precision
HDI boards require tight manufacturing tolerances because small dimensional variations can affect circuit performance.
Manufacturers should be capable of producing fine traces, accurately positioned microvias, and properly aligned multilayer structures.
Engineering Support
Engineering communication plays an important role in preventing design-related manufacturing problems.
A manufacturer that provides clear design feedback can help customers identify potential fabrication limitations and improve production readiness.
Quality Management
Consistent quality control is essential for reducing manufacturing defects and maintaining product reliability.
Customers should evaluate inspection methods, testing procedures, documented quality practices, and relevant certifications.
Prototype and Production Capabilities
Businesses often begin with small prototype quantities before transitioning to larger production orders.
A manufacturing partner capable of supporting different production stages can help simplify supplier coordination.
Communication and Delivery Planning
Clear communication helps customers understand technical requirements, manufacturing schedules, and potential production challenges.
Reliable delivery planning is especially important for companies working with demanding product development timelines.
The Importance of Prototype Development in HDI PCB Manufacturing
Prototype development is an essential stage in bringing advanced electronic products to market.
Before committing to larger production quantities, engineers must verify that their PCB designs function as intended.
HDI PCB prototypes help businesses evaluate:
- Electrical connectivity and circuit functionality.
- Signal integrity and high-speed performance.
- Component compatibility.
- Thermal behavior under operating conditions.
- Mechanical dimensions and assembly requirements.
- Manufacturing feasibility.
- Potential design improvements.
FastTurn PCBA’s PCB manufacturing and assembly solutions can support businesses during the transition from design evaluation toward production.
Early prototype testing can help identify problems that would otherwise become expensive during larger manufacturing runs.
Common Challenges in HDI PCB Manufacturing
Although HDI technology provides substantial design advantages, it also introduces manufacturing challenges.
Understanding these challenges helps engineers develop more reliable products.
Microvia Reliability
Microvias must maintain dependable electrical connections despite thermal and mechanical stresses.
Appropriate design rules, plating quality, and manufacturing controls are important for reducing reliability risks.
Layer Alignment
Complex multilayer boards require precise registration between conductive layers.
Poor alignment can create connection problems and reduce manufacturing yield.
Thermal Management
Dense component placement may increase localized heat generation.
Engineers must consider copper distribution, thermal vias, material properties, and cooling requirements when developing HDI designs.
Manufacturing Costs
Advanced drilling, fine-line processing, and sequential lamination can increase manufacturing complexity.
However, HDI technology may also provide system-level benefits by reducing board dimensions or enabling more compact product architectures.
Design Complexity
HDI boards often require specialized layout techniques and careful coordination between design engineers and manufacturers.
Early communication can help prevent unnecessary revisions and improve production efficiency.
How FastTurn PCBA Supports Advanced Electronic Development
FastTurn PCBA offers PCB manufacturing and assembly solutions for businesses seeking to develop advanced electronic products.
By addressing fabrication and assembly requirements within the production workflow, the company provides a practical option for organizations working with sophisticated PCB designs.
Businesses considering FastTurn PCBA for HDI projects should communicate their technical requirements clearly, including board stack-up, microvia structures, material specifications, component density, testing expectations, and production quantities.
This information allows the manufacturer to evaluate project feasibility and determine suitable manufacturing approaches.
For complex electronic applications, cooperation between PCB designers and manufacturing teams can help improve production readiness and reduce avoidable technical difficulties.
Future Trends in HDI PCB Technology
The demand for HDI printed circuit boards is expected to remain closely connected to advances in electronic miniaturization and high-performance computing.
Several developments are shaping the future of HDI technology.
Increasing Electronic Miniaturization
Manufacturers continue to develop smaller electronic products with more advanced capabilities.
This trend creates additional demand for compact PCB structures that support dense component placement.
Advanced Semiconductor Packaging
Sophisticated semiconductor packages require increasingly complex interconnection structures.
HDI technology helps PCB designers accommodate fine-pitch components and advanced electronic architectures.
High-Speed Communication Systems
Modern communication technologies place greater demands on signal integrity and circuit board design.
Advanced PCB materials and high-density routing techniques will remain important for supporting high-speed electronic systems.
Improved Manufacturing Automation
Automated inspection, advanced imaging, and more precise production equipment can help manufacturers improve consistency and reduce manufacturing defects.
Growing Demand for Reliable Electronics
Industries such as medical technology, automotive electronics, industrial automation, and telecommunications increasingly depend on compact electronic systems.
HDI technology provides valuable design capabilities for meeting these evolving requirements.
Conclusion
High-Density Interconnect technology plays an essential role in modern electronics by enabling compact circuit layouts, sophisticated component integration, and advanced electrical performance. From consumer electronics and medical devices to telecommunications and industrial automation, HDI printed circuit boards help manufacturers address increasingly complex design requirements.
Selecting a dependable hdi pcb manufacturer is an important step toward achieving reliable electronic product development. Manufacturing precision, engineering support, quality management, and production flexibility all influence the success of an HDI PCB project.
FastTurn PCBA provides PCB manufacturing and assembly solutions for businesses developing advanced electronic applications. By focusing on technical requirements, manufacturing coordination, and quality considerations, FastTurn PCBA offers a valuable option for companies seeking efficient circuit board production.
As electronic devices continue to become smaller and more sophisticated, HDI PCB technology will remain an important foundation for innovation, helping businesses develop reliable and competitive electronic products.


-
 Celebrity1 year ago
Carolin Bacic: Life, Biography, Family, and Legacy
-
 Celebrity9 months ago
Alex Eala: Rising Tennis Star from the Philippines and Her Journey to Global Success
-
 Celebrity2 years ago
Christine Williamson: A Rising Star in Sports Journalism
-
 Celebrity1 year ago
Dani Daniels: A Complete Biography of the Artist, Media Personality, and Entrepreneur
-
 Celebrity8 months ago
Valerie Perrine: A Complete Biography of the Acclaimed Actress and Icon
-
 Celebrity1 year ago
Eleonora Incardona: Biography, Career, Age, Boyfriend, Net Worth & Lifestyle (2025)
-
 Celebrity2 years ago
Vera Davich: Biography, Life, and Legacy2025
-
 Celebrity1 year ago
Ari Kytsya: Biography, Career, Age, Lifestyle & Rise as a Global Social Media Star